
Views: 0 Author: Site Editor Publish Time: 2026-09-16 Origin: Site


Picture this: You just spent six hours meticulously blocking and prepping a panel. You lay down the perfect base coat, only to watch in absolute dismay as crater-like fisheyes and dust nibs ruin the final clear coat. Straight compressed air is inherently hot, wet, and loaded with microscopic debris. Consequently, a highly engineered pneumatic purification system serves as your ultimate line of defense.
In this comprehensive guide, we will explore the exact purity standards required for flawless finishes. From an engineering standpoint, we will detail how to configure the optimal pneumatic setup to protect your shop's throughput and profit margins.
When evaluating the success of a finishing project, technicians often prioritize the mechanical tuning of the spray gun and the chemical composition of the coating. However, the pneumatic medium delivering that material is equally critical. Operating without a dedicated filtration system introduces severe, often irreversible risks to the final finish. Ignoring compressed air quality will inevitably lead to compounding rework, squandered labor hours, and wasted materials.
Air compressors ingest ambient shop air, which naturally harbors dust, humidity, and microscopic debris. Upon compression, the concentration of these impurities skyrockets. If left unchecked, they manifest as distinct, recognizable defects on the workpiece.
For instance, fisheyes—small, crater-like openings in the finish—are almost exclusively caused by silicone or oil aerosols traveling through the line. Because lubricated compressors naturally produce blow-by, these microscopic oil droplets mix with the paint and actively repel the coating. Blistering and blushing (cloudiness) occur when airborne vapor cools and condenses inside the hose. When this liquid water mixes with solvent-based or waterborne paints, it traps moisture under the curing surface. Finally, solid particulates like ambient pollen and internal pipe scale create physical bumps, or nibs, ruining the glass-like smoothness expected in premium clear coats.
Automotive refinishing is rapidly shifting towards waterborne basecoats due to tightening global VOC (Volatile Organic Compound) regulations. From a technical perspective, these modern water-based formulations are exceptionally unforgiving when exposed to pneumatic impurities. Even a fraction of a drop of compressor oil will cause massive coating failure. This industry-wide trend makes high-grade, multi-stage filtration not just an optional upgrade, but a mandatory survival tool for modern body shops.
To achieve professional-grade results, "clean" cannot remain a subjective term. The manufacturing and refinishing industries rely on empirical data and international benchmarks to define exact purity levels.
The International Organization for Standardization established the ISO 8573-1 framework to classify pneumatic purity. This standard measures three specific contaminants: solid particulates, water, and oil. For high-end automotive painting and sensitive industrial coatings, the supply must generally meet ISO 8573-1 Class 1 or Class 2 for both oil and particulates, and at least Class 4 for water. Reaching this clinical level of highly purified air is impossible straight from a receiver tank. It demands a highly engineered, multi-stage setup designed to intercept microscopic threats.
Understanding how these impurities form is the crucial first step to eliminating them. First, the compression process generates immense thermal energy. As hot air leaves the pump and travels down the piping, it begins to cool rapidly. This temperature drop lowers the air's capacity to hold moisture, causing vapor to condense into liquid pooling. Second, oil-injected rotary screw or reciprocating compressors utilize lubricants for sealing and cooling. Despite internal separators, trace amounts of aerosolized oil inevitably escape downstream. Lastly, the internal environment of a pneumatic system degrades over time. Moisture causes steel tanks and iron pipes to oxidize, propelling rust flakes toward your nozzle at high velocities.
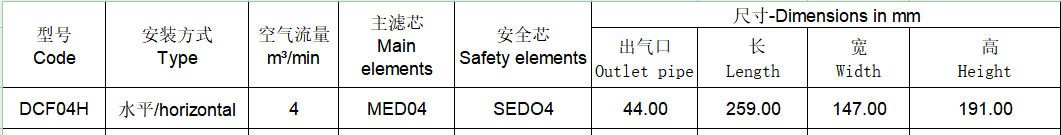
A specialized spray gun filter is a precision pneumatic device. It is engineered to strip solid, liquid, and vaporous contaminants from the stream immediately before the fluid enters the atomization chamber.
While designs vary across manufacturers, enterprise-grade assemblies—such as the advanced DCF Series—share specific industrial characteristics. They typically feature a robust die-cast aluminum housing capable of withstanding dynamic pressures up to 1.6 MPa (232 PSI). Internally, they utilize a directional baffle, a specialized media element (often crafted from sintered bronze or borosilicate glass microfibers), and an automatic float drainage mechanism at the base of the bowl. As compressed air enters the housing, it is forced through the media, which acts as a physical barrier. The purified air continues to the outlet, while trapped debris and liquids fall into the collection bowl.
Achieving ISO-certified purity requires multiple stages. No single element can simultaneously catch bulk water, heavy rust, and ultra-fine aerosols.
Particulate Filters serve as the first line of defense. They utilize a porous element (usually rated between 5 and 40 microns) to capture large solid debris. Often combined with this first stage, a cyclonic separator employs an internal baffle to spin the incoming flow. This centrifugal force throws heavy liquid droplets against the outer wall, where they slide into the drain.
In contrast, standard mechanical traps cannot catch fine mists. This is where Coalescing Filters become mandatory. Utilizing a dense matrix of micro-fibers (typically rated at 0.01 microns), they force microscopic oil and water aerosols to collide. These aerosols merge into larger droplets until they are heavy enough to fall. This final stage is absolutely critical for flawless spray painting.
Selecting the correct equipment requires matching the technical specifications of the unit to the specific volumetric demands of your compressor and spray tools. High-efficiency paint filtration prevents catastrophic coating failures, but only if sized correctly.
| Filter Stage | Micron Rating | Primary Function | Best Application Location |
|---|---|---|---|
| Stage 1: Particulate / Water Trap | 5 to 40 Microns | Removes bulk liquid water, rust scale, and large dust. | Wall-mounted, at least 25 feet downstream from the compressor. |
| Stage 2: Coalescing Filter | 0.01 Microns | Strips microscopic oil aerosols and ultra-fine moisture mist. | Wall-mounted, immediately following the Stage 1 trap. |
| Stage 3: Desiccant Dryer (Optional but Recommended) | N/A (Chemical) | Absorbs invisible water vapor, lowering the dew point. | Wall-mounted, specifically for dedicated paint booth lines. |
| Final Stage: Inline Mini Filter | Variable | Catches residual hose debris (rubber flakes) right before atomization. | Threaded directly onto the base of the spray gun. |
When evaluating a purchase, the Cubic Feet per Minute (CFM) rating is paramount. High-Volume Low-Pressure (HVLP) guns require a massive volume to atomize correctly—often between 12 and 16 CFM. If your filtration unit is only rated for 10 CFM, it will create a severe bottleneck. This starves the tool, resulting in a poorly atomized, heavily textured finish (orange peel). Always verify that the housing's flow capacity exceeds your tool's maximum requirement by at least 20% to account for dynamic pressure drops across the filter media.
Even the most expensive multi-stage system will fail spectacularly if installed incorrectly. The thermodynamics of compressed air dictate strict rules for piping and placement.
We constantly see shops making the mistake of mounting the primary unit directly next to the compressor pump. When air leaves the pump, it is incredibly hot, meaning moisture exists purely as a vapor. Because mechanical traps cannot catch vapor, you must follow the "cooling rule." Wall-mounted units should be installed a minimum of 25 to 50 feet downstream. This distance allows the hot air to travel through the metal piping and cool down to ambient room temperature. Consequently, the vapor condenses into liquid droplets that the filter can actually separate.
To ensure optimal performance, always use rigid hard piping like copper, aluminum, or specialized pneumatic tubing. Avoid PVC (which is a severe shatter hazard) and standard black iron (which rusts profusely). Furthermore, never pull air from the bottom of a main pipe run. Instead, plumb a "T" fitting that pulls from the top of the pipe, routing it down to your housing. Below this junction, install a downward drip leg with a manual ball valve to catch bulk water before it ever reaches the filter media. Finally, verify the airflow direction arrows stamped on the housing; installing a unit backward will instantly destroy the element.
Media elements are strictly consumable items. Over time, the microscopic pores become permanently saturated with oil, water, and dirt. If neglected, this leads to inevitable system failure.
Do not wait for a ruined clear coat to inspect your setup. Monitor your system for telltale failure indicators. If you set your regulator to 29 PSI, but it plummets to 15 PSI the moment you pull the trigger, the element is likely clogged and restricting flow. Additionally, utilize visual indicators. High-end coalescing units often feature differential pressure gauges that transition from green to red as they clog. If you notice an oily film inside your hose, a breach has already occurred.
While maintenance schedules depend heavily on run time and ambient humidity, standard industry baselines provide a safe starting point. Standard 5-micron particulate elements require monthly inspection and replacement every six months. Crucially, 0.01-micron coalescing elements should be swapped every three to six months. Once a borosilicate glass element is saturated with compressor oil, it cannot be recovered.
A prevalent debate in automotive forums centers on saving money by blowing out a dirty paper or synthetic element with compressed air. The objective, scientific answer is no. Filtration media relies on a highly precise, microscopic web of fibers to trap particles. Blasting this delicate structure with 90 PSI tears the fibers apart. While it may look cleaner to the naked eye, you have effectively blown microscopic holes straight through the barrier. This guarantees that contaminants will pass through during your next paint session. Always replace; never blow out.
Even with a robust installation, environmental factors or mechanical wear can occasionally cause defects. Adopting a systematic, evidence-based approach to diagnostics is crucial to pinpoint the exact point of failure.
Water remains the most pervasive contaminant in any pneumatic circuit. If micro-pinholes appear in your clear coat, liquid water is actively bypassing your defenses. Begin by inspecting the automatic drain mechanisms. A high-quality moisture separator utilizes internal floats to discharge collected water. If this float becomes clogged with rust scale or emulsified oil sludge, the bowl will fill completely. High-velocity air will then pick the resting water back up and carry it straight into your hose. Additionally, evaluate extreme ambient temperature fluctuations. If the shop temperature drops significantly overnight, the metal piping acts as a heat exchanger, causing spontaneous condensation downstream of your wall units.
A flawless finish relies on precise atomization, which requires stable dynamic pressure. Pressure drops are almost always caused by a physical restriction in the airflow path. When diagnosing this, saturated filter elements are the primary suspect. As solid particulates permanently blind the microscopic pores of a coalescing filter, the effective surface area shrinks, forcing a significant loss of downstream pressure. Alternatively, inspect the regulator itself. Over time, chemical degradation can stiffen the internal rubber diaphragm, preventing the valve from opening fully when dynamic flow is demanded.
Before mixing your paint, perform a simple baseline test. Take a clean mirror, a piece of glass, or specialized air quality test paper. Hold your spray gun (without the paint cup attached) about two inches away from the surface and blast straight air at 90 PSI for 30 to 60 seconds. Inspect the surface closely under good lighting. Any condensation rings, water droplets, or oily smudges indicate that your filtration system has been breached and requires immediate maintenance.
Spraying clear coat with raw, unfiltered air almost guarantees a compromised finish. You will likely experience severe solvent pop, micro-blistering, and fisheyes as oil aerosols actively repel the clear coat resins. Additionally, microscopic rust and dust from the piping will embed into the wet clear, creating a rough, textured surface (nibs) that requires hours of aggressive wet sanding and compounding to correct.
Yes, it is absolutely mandatory for professional applications. Draining your tank daily is a critical habit, but it only removes "bulk water"—the liquid that has already precipitated and pooled at the bottom. The air sitting above that bulk water remains at 100% relative humidity. As this highly saturated air leaves the tank and travels down your piping, it continues to cool, forcing suspended vapor to condense into new liquid droplets directly inside your lines. A dedicated separator is required to intercept this newly formed condensation.
No, relying on a standard tool filter for fine-finish work is a critical error. Standard units, often rated at 40 microns, are designed exclusively to catch large solid debris and heavy liquid water to prevent impact wrenches from seizing. They cannot stop microscopic oil aerosols or fine water mists. Lubricated compressors constantly bypass a fine mist of oil (often smaller than 1 micron) into the airstream. To safely atomize coatings, you must use a setup that includes a 0.01-micron coalescing element.
There is no single "best" micron rating, as proper purification requires a staged methodology. The first stage should be a 5-micron particulate filter and water trap to knock out bulk liquid, pipe scale, and large dust. The second stage must be a 0.01-micron coalescing filter, which is then free to focus entirely on trapping microscopic oil aerosols and ultra-fine moisture vapor without becoming prematurely clogged by large debris.
A disposable inline unit must be attached directly to the base of the paint gun, serving as the absolute final point-of-use defense. It should be threaded into the air inlet, immediately preceding the mini regulator. This location is critical because flexible rubber hoses degrade over time due to UV exposure and physical wear, shedding microscopic rubber flakes directly into the clean airstream. Placing the inline filter directly on the tool intercepts any debris generated by the hose itself.
Ultimately, the structural integrity and aesthetic perfection of your finishing project rely entirely on the purity of your pneumatic supply. Operating a bare compressor guarantees ruined finishes, frustrating rework, and wasted materials. By installing a reliable, multi-stage filtration system, you actively protect your hard work from the devastating effects of microscopic oil, water, and particulates.
Do not gamble with your next professional project. If you are experiencing inconsistent finishes or frequent pressure drops, it is time to evaluate your pneumatic infrastructure. Upgrade your shop today with industrial-grade, ISO-compliant purification solutions from Sykingtech to ensure a flawless, glass-like finish every single time.
